Products · Studs
Engineer studs
Double-ended engineer studs for tapped holes, made to DIN, BS and NFE standards or your drawing, including larger diameters, longer lengths and through-drilled studs.
DIN 938
Plus DIN 939, DIN 940 and BS 2693
1 to 500
Single prototypes to batches of several hundred
UK, EU, US
Mill origin of every bar we use
3.1 / 3.2
EN 10204 certificates with full traceability
About Engineer studs
Larger, longer and drilled studs are our niche
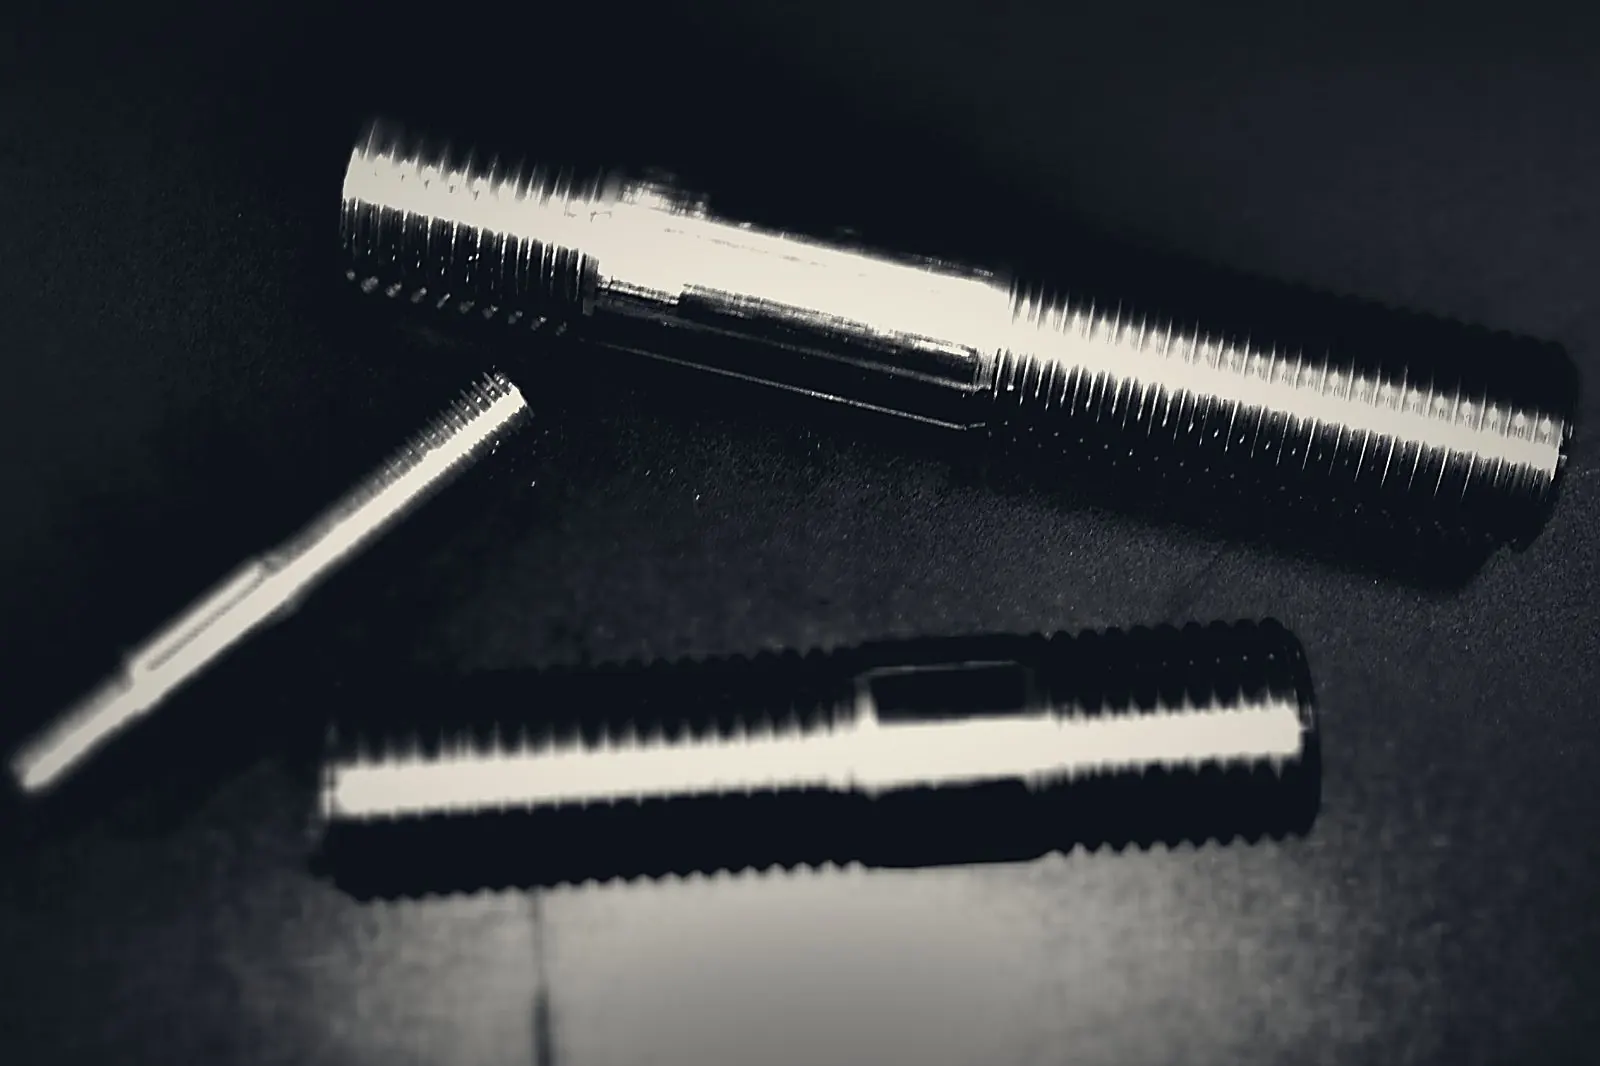
Engineer studs are threaded at both ends with a plain shank in the middle. One end screws permanently into a tapped hole in a casting or housing, and a nut on the other end clamps the cover or flange. HAGUE FASTENERS makes engineer studs in the UK, specialising in larger diameters, longer lengths and through-drilled studs.
Our experience shows in high temperature grades, super duplex and critical stainless steels, where engineer studs hold together turbines, valves, pumps and engines that run hot or in corrosive conditions.
Where engineer studs are used
- Pump, valve and compressor casings
- Turbine and engine cylinder heads
- Gearbox and bearing housings
- Manifolds and exhaust flanges
- Heavy castings that must not be re-tapped
Options
Typical specifications
Typical options. We make to the standard or drawing you specify.
| Option | What we make |
|---|---|
| Metal end | Length to suit the tapped material, for example 1d, 1.25d or 2.5d to DIN 938, 939 and 940 |
| Form | Plain or reduced shank, through drilled on request |
| Thread | Metric coarse and fine, UNC, UNF, UN, BSW, BSF and special forms, cut or rolled |
| Strength | Classes 8.8, 10.9, 12.9 and 14.9; ASTM A193 B7, B16, B8 and B8M; A320 L7 |
| Standards | DIN 938, DIN 939, DIN 940, BS 2693, BS 4439, NFE 25135 |
| Finishes | Self colour, zinc, zinc nickel, zinc flake (Geomet, Delta Protekt), hot dip galvanising, electroless nickel, PTFE fluoropolymer, phosphate or passivation |
| Documentation | Certificate of conformity, EN 10204 3.1 or 3.2, test reports, dimensional reports and FAIR |
Materials
Materials we use
Certified bar from UK, EU and US mills. See all fastener materials.
- Carbon and alloy steels: B7, L7, B16, BS 4882 B16A, EN24 and 42CrMo4
- Stainless steels: B8, B8M, B8T, 316, 17-4PH and A453 660
- Duplex and super duplex: S31803, S32750, S32760 and Zeron 100
- Inconel: 625 and 718
- Incoloy: 825 and A286
- Monel: 400 and K500
- Hastelloy: C276 and C22
- Titanium: titanium alloys
Manufacture and quality
Made in Willenhall, certified to release
Turned and threaded in our own Willenhall facility, with batches on automatic bar machines, from certified UK, EU and US bar.
- Heat numbers traced from mill to release
- Heat treatment, NDT and coating by approved partners
- UKAS-accredited testing where specified
Questions
Frequently asked questions
What is an engineer stud?
An engineer stud is threaded at both ends with a plain centre. One end screws into a tapped hole and stays there; a nut on the other end clamps the joint.
What is the difference between DIN 938, 939 and 940?
They differ in the length of the metal end: about 1 times the diameter for DIN 938, 1.25 times for DIN 939 and 2.5 times for DIN 940, to suit steel, cast iron and softer metals.
Can you make through-drilled engineer studs?
Yes. Through-drilled engineer studs, larger diameters and longer lengths are a speciality.
Do you make engineer studs in high temperature grades?
Yes. We make engineer studs in B16, A453 660, Nimonic 80A, Inconel 718 and other high temperature grades.
Useful tools
Free engineering tools
- Bolt torque calculator: tightening torque and preload for metric, UNC, UNF, BSW and BSF threads.
- Stud bolt weight calculator: weigh studs and nuts for one piece or a whole order, in kg and lb.
- Thread size chart and identifier: pitch, diameters, stress area and tapping drill, or identify an unknown thread.
Free to use, no sign-up. See all our engineering tools.
Engineer stud enquiry?
Send us the drawing or the standard
Tell us the size, both thread lengths, grade and quantity, and we will quote quickly.